


HMEF (Heat and Moisture Exchange Filter) is a core medical consumable specifically designed for patients with artificial airways, integrating heat and moisture recovery with filtration and protection. Suitable for mechanical ventilation or spontaneous breathing support scenarios, it efficiently retains heat and moisture from exhaled gas to humidify and warm inhaled air, while filtering pathogens and particles. It not only optimizes airway care effectiveness but also reduces the risk of cross-infection, making it an essential medical device in ICUs, operating rooms, emergency departments, and home care settings.
Core Features

Efficient Heat and Moisture Exchange: Adopting highly absorbent medical fiber materials, it can recover ≥85% of heat and moisture from exhaled gas, providing inhaled air with a temperature and humidity close to physiological conditions. This reduces airway mucosal dryness, damage, and sputum scab formation, enhancing patient comfort.
Dual Protection Filtration: Equipped with a HEPA-grade filter layer, it can block ≥99.9% of particles ≥0.3μm, as well as pathogens such as bacteria and viruses. It provides two-way protection for patients and medical staff, lowering the risk of nosocomial infections.
Universal Compatibility: Featuring a standardized interface design, it is compatible with various endotracheal tubes, tracheostomy tubes, and ventilator circuits. Suitable for adults, pediatric patients, and infants, it can be installed easily without additional tools.
Safe and Comfortable Materials: Made of medical-grade non-toxic and odorless materials, its biocompatibility complies with ISO 10993 standards. It is hypoallergenic with a smooth and soft surface, minimizing irritation to the airway mucosa.
Lightweight and Durable Design: The product weighs only 5-12g and has a compact size (5×3×2cm), without adding burden to the patient's airway. The single-channel airflow design ensures low resistance (≤3cmH₂O) and does not affect ventilation efficiency.
Product Specification
|
Item |
Specification |
|
Compatible Populations |
Adults, pediatric patients, infants |
|
Material |
Medical-grade fiber filter paper, ABS shell, silicone gasket |
|
Heat and Moisture Exchange Efficiency |
≥85% |
|
Filtration Efficiency |
≥99.9% for particles ≥0.3μm |
|
Operating Temperature |
-5℃~40℃ |
|
Relative Humidity Tolerance |
10%~95% |
|
Service Life |
Single-use: 24 hours; Reusable: 7 days (after EO sterilization) |
|
Sterilization Method |
EO-sterilized (supplied sterile) |
Product Properties

- Hospital Settings: Used for airway care of mechanically ventilated patients in ICUs, operating rooms, and respiratory wards.
- Emergency Rescue: Applied in ambulances and emergency departments to provide temporary airway protection and temperature-moisture support for patients with respiratory failure.
- Home Care: Suitable for home rehabilitation patients after tracheotomy, simplifying the airway care process.
- Primary Medical Institutions: Meets the nursing needs of patients with respiratory diseases in community hospitals and clinics.

Storage and Usage Instructions
Storage: Store in a sealed, clean, dry, and well-ventilated environment. Avoid direct sunlight, high temperatures, contact with sharp objects, and corrosive substances. Keep single-use products sealed until use.
Usage: For single-use HMEFs, discard immediately after use to prevent cross-infection. For reusable versions, sterilize by EO after each use and inspect for damage, filter contamination, or seal defects before reuse. Avoid touching the inner surface of the filter that contacts the patient's airway to maintain sterility.
Quality Assurance: Complies with ISO 13485, CE, and NMPA medical device standards. Each batch undergoes strict testing, including heat-moisture exchange efficiency verification, filtration performance testing, leak testing, and biocompatibility assessments. A unique batch number is assigned for full traceability, and a detailed Instruction for Use (IFU) is provided.

Packing,Storage,Handling and Transportation
Packing:
Single-use versions: Individually packaged in EO-sterilized paper-plastic composite bags, with a waterproof, dustproof storage pouch included. Each package is printed with product information, sterilization date, batch number, and expiration date.
Reusable versions: Packaged in PE bags with sterilization indicators, accompanied by a cleaning and sterilization guide.
Bulk transport: Packed in sturdy corrugated cartons with anti-crush buffers (e.g., bubble wrap, pearl cotton) to prevent structural damage during transportation. Each carton is labeled with product name, specification, quantity, batch number, and "Medical Device" warning signs.
Storage:
Store in a clean, dry, well-ventilated warehouse with a temperature of -5℃~40℃ and relative humidity ≤80%.
Avoid direct sunlight, high temperature, high humidity, and contact with sharp objects, corrosive substances (e.g., acids, alkalis), and volatile chemicals.
Keep single-use products sealed until use; do not open the package in non-sterile environments.
Stack cartons no more than 10 layers to prevent crushing the products inside.
Handling:
Single-use products: Discard immediately after use; do not reuse, disinfect, or repackage to avoid cross-infection.
Reusable products: After use, clean thoroughly to remove debris and secretions, then sterilize by EO or autoclave (134℃, 20 minutes). Inspect for cracks, filter contamination, interface damage, or sealing ring aging before reuse; discard if any defects are found.
Avoid touching the filter layer and inner surface of the product during handling to maintain sterility.
Transportation:
Transport in accordance with national and international medical device transportation regulations, avoiding violent collision, jolting, rain, or moisture.
Use refrigerated or insulated vehicles for transportation in extreme temperature environments (below -5℃ or above 40℃) to ensure product performance is not affected.
The transportation process shall be recorded, including departure date, destination, transportation conditions, and receiver information, for traceability.
Reasons for choosing us
Zhejiang Mediunion Healthcare Group Co. Ltd. (a branch of Evergrand Healthcare Group, founded in 2014) is located in Ningbo City, Zhejiang Province - enjoying an excellent location and convenient transportation. Our business covers medical device manufacturing & sales, plus investments in nursing homes, dental clinics, specialist hospitals and medical care services. Our products are sold worldwide, and we've won global consumer recognition with high-quality goods and comprehensive after-sales service.
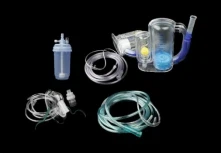
Diversified Product Portfolio
Our product range includes disposable medical consumables, medical equipment and non-woven products (e.g. dental supplies, respiratory care items). This diverse lineup caters to the needs of medical institutions, clinics and other clients.
Reliable Supply & Collaboration
We have rich industry experience and partner with over 600 factories. These partners are equipped with advanced production equipment and skilled frontline staff, enabling us to produce customized products/components as per specific requests.

Strict Quality Assurance
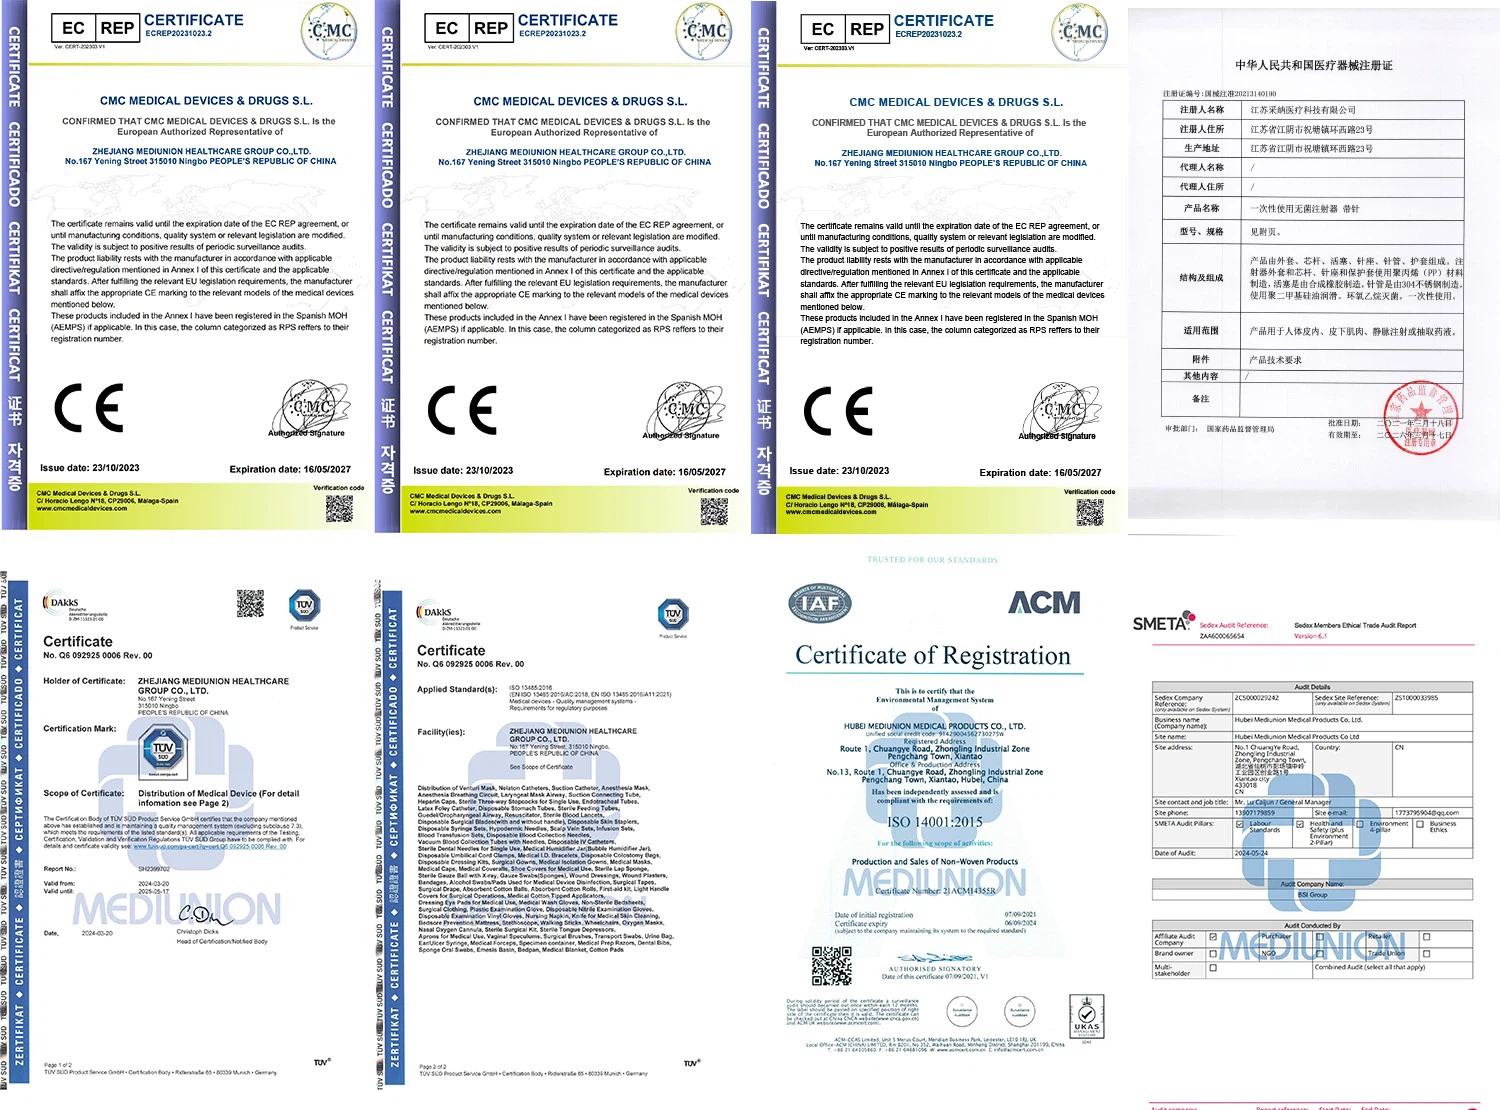
We prioritize innovation & quality, backed by the ISO 13485:2016 quality management system. Strict control runs through raw material procurement, mass production, process management and finished product release. Our professional services (production control, order follow-up, delivery) also set us apart.
Certificate
FAQ
Q:What is your quality control process from raw material to finished goods?
A:Our quality control process is comprehensive and covers the entire supply chain:
Incoming Raw Material Inspection: All raw materials are tested against specified standards (e.g., purity, biocompatibility) with COA verification before entering production;
In-Process Quality Control: Key production stages are monitored in real-time, with sampling inspections for critical parameters to prevent deviations;
Finished Goods Inspection: 100% visual inspection and random sampling for performance, sterility (if applicable), packaging integrity, and labeling compliance;
Post-Production Traceability: Each batch is assigned a unique traceability code, linking raw materials, production records, and test results for full traceability.
Q:How do you ensure batch-to-batch consistency?
A:We ensure batch-to-batch consistency through:
Standardized production processes (SOPs) strictly followed by trained operators;
Calibrated and maintained production equipment to ensure stable performance;
Routine testing of critical quality attributes across batches;
Statistical Process Control (SPC) to monitor and adjust production parameters in real-time;
Regular review of batch records and quality data to identify and address potential variations.
Q:Can you provide COA, test reports, and traceability records?
A:Yes, we can provide Certificate of Analysis (COA) for each batch, detailed test reports (including raw material tests, in-process tests, and finished product tests), and complete traceability records. These documents include information such as raw material suppliers, production dates, batch numbers, test results, and inspection signatures, ensuring full transparency and traceability.
Hot Tags: hmef, China hmef manufacturers, suppliers, factory, respiratory nebulizer, high flow cannula, Disposable Transparent CPR Mask, respiratory therapy mask, PVC Manual Resuscitator, Silicon Manual Resuscitator


